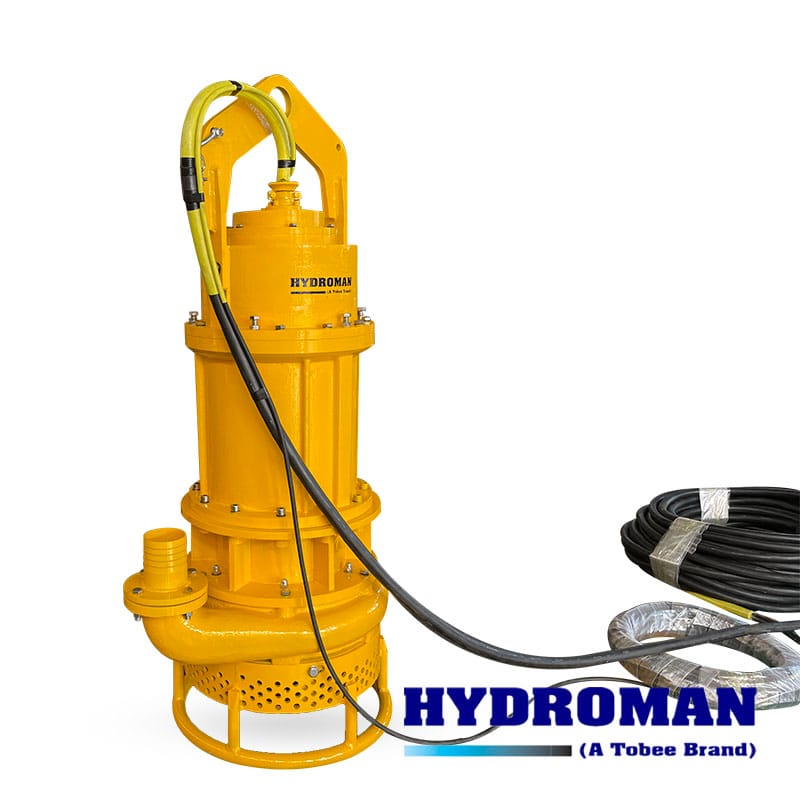

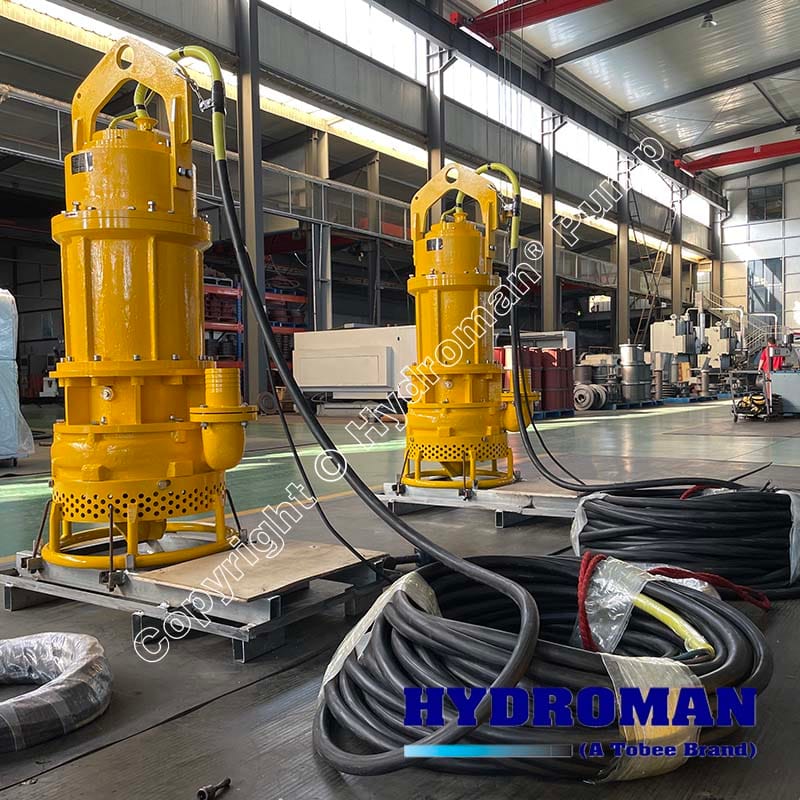

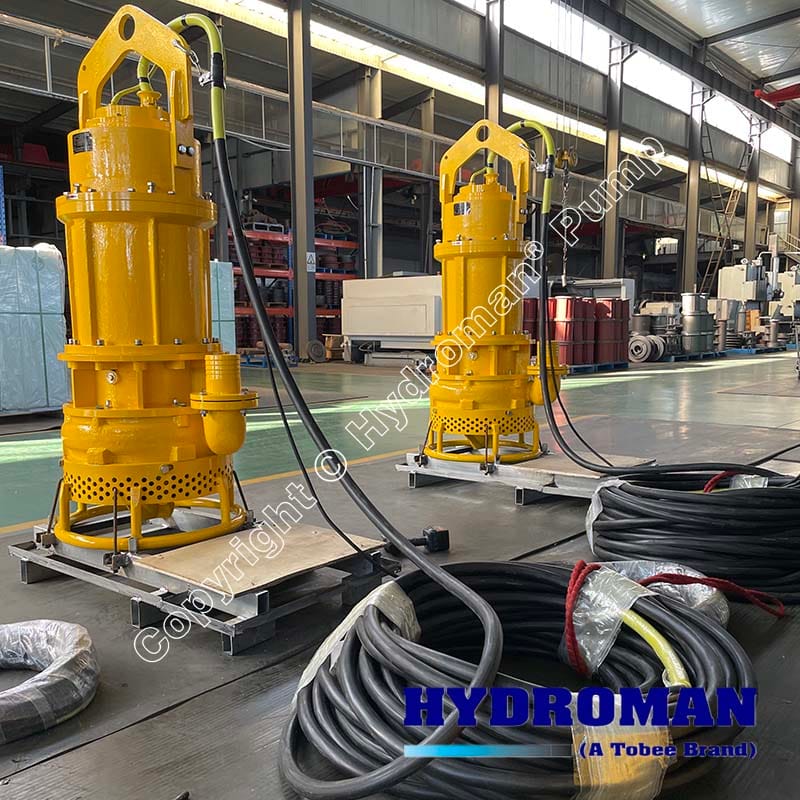
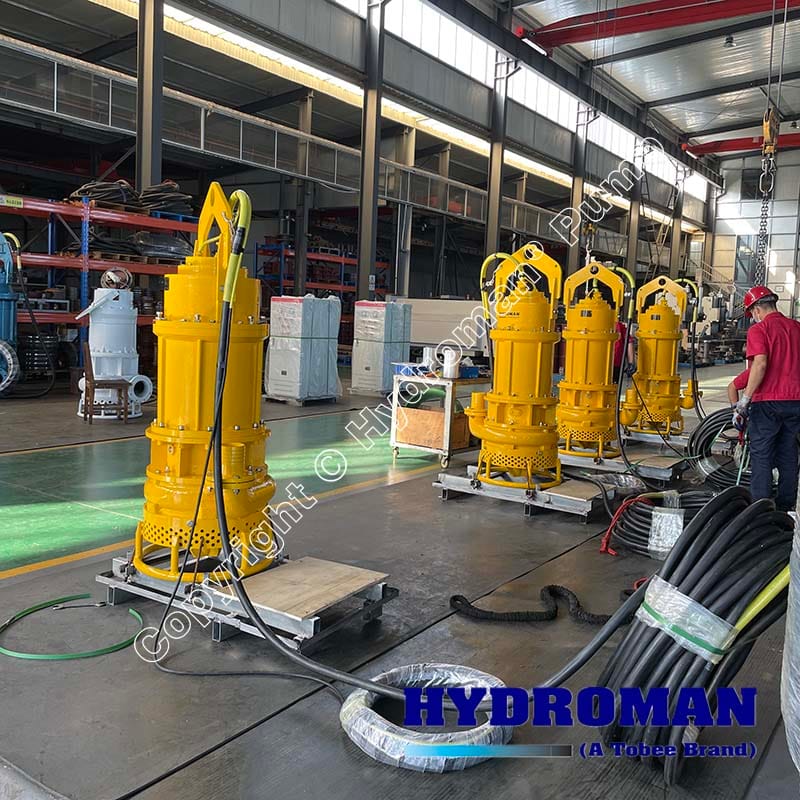
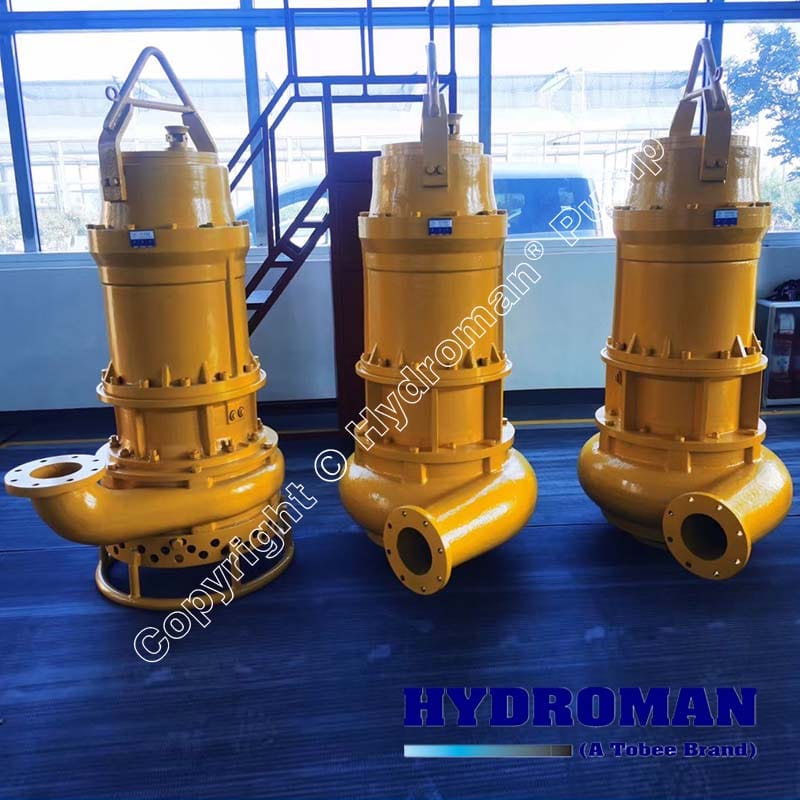
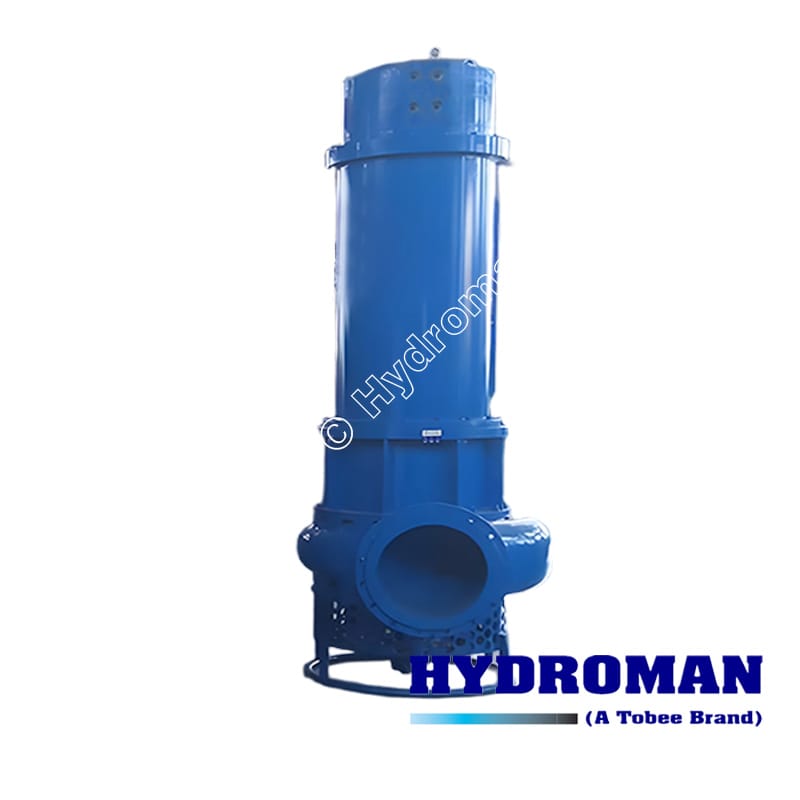
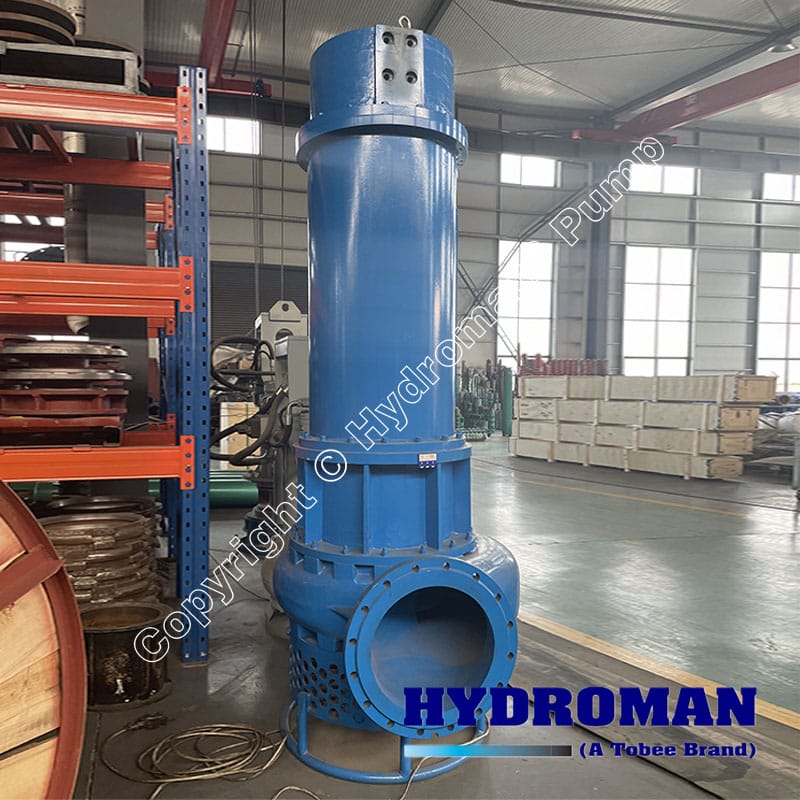
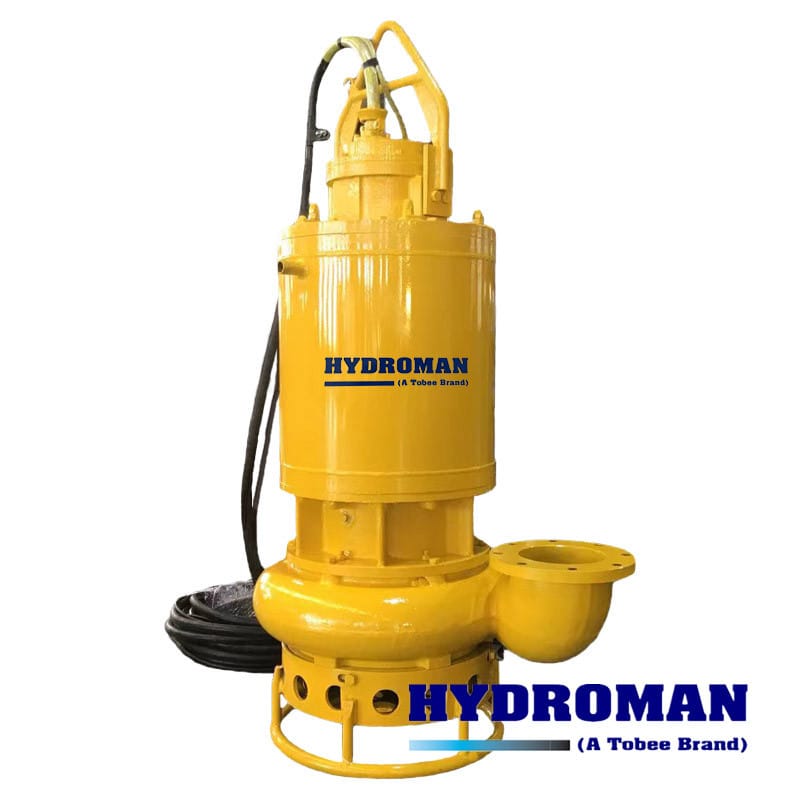
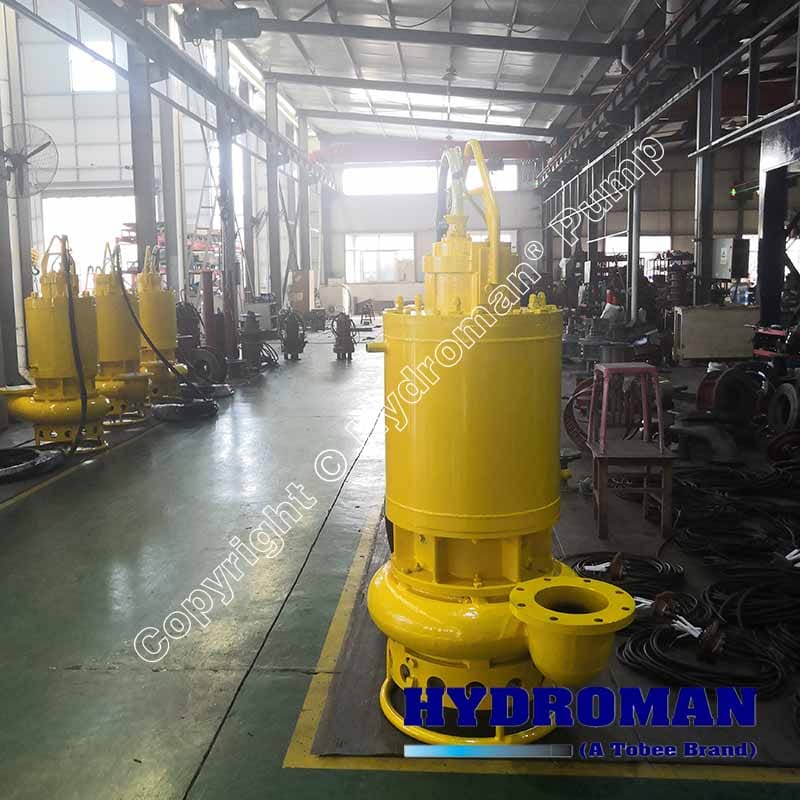
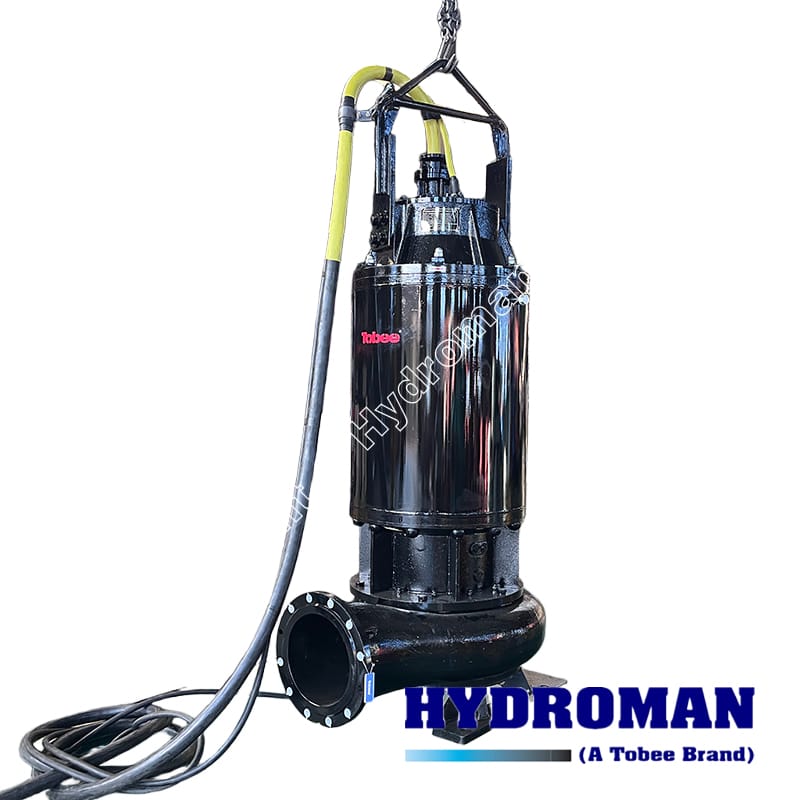
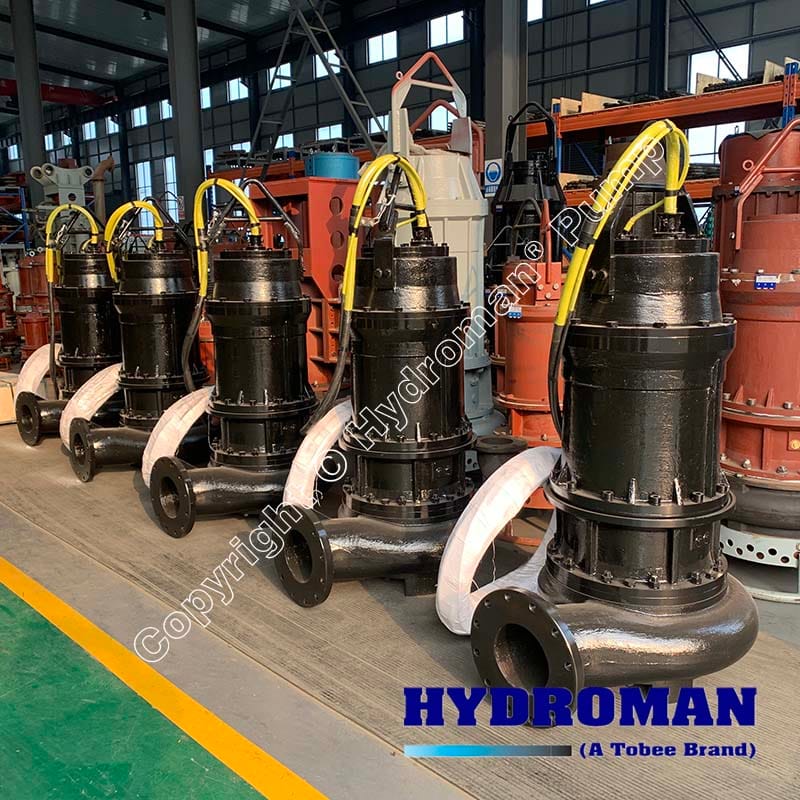
• Hydroman® Submersible Slurry Mud Pump is famous for its dependable and energy saving perfomance all over of drainage projets.
• The Slurry Mud Removal pumps is driven by electricity and suggest you verically use, which can supply valid pumping of corrosion and abrasion slurris and mud.
• Designing a unity of Hydroman hyperchrome alloy casting for highy abrasive resistance and a suction filter to prohibit extremely big solids blocking the pump. These submerisble mud pumps guarantee high uptime.
• Longer wear resistant lifetime and valid pumping of highly-centralized and corrosive slurries
• Capable of transporting between 7m3/h and 2400m3/h, up to 120m head and 120mm particles
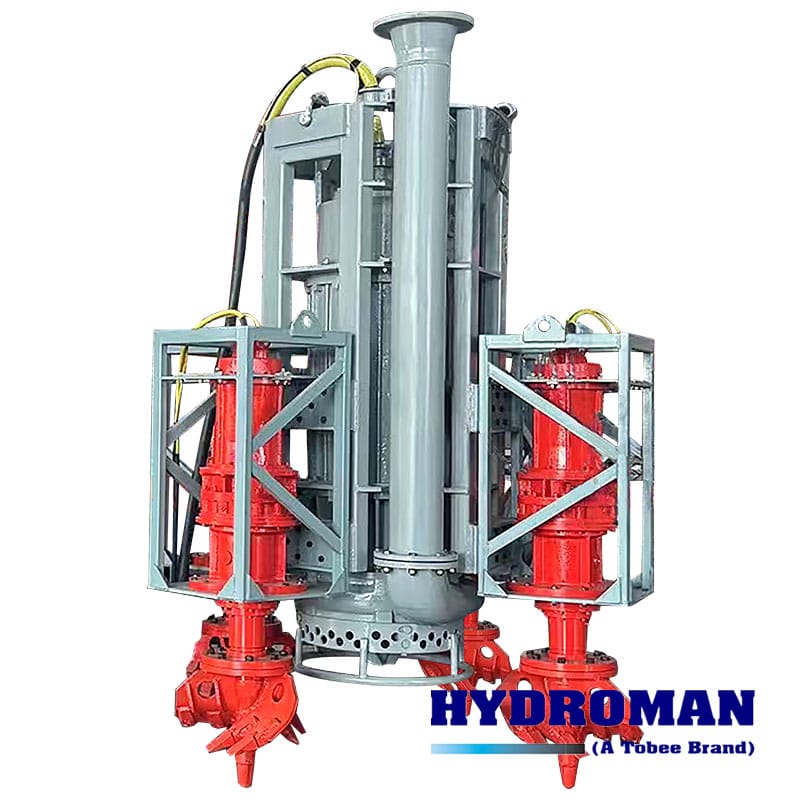
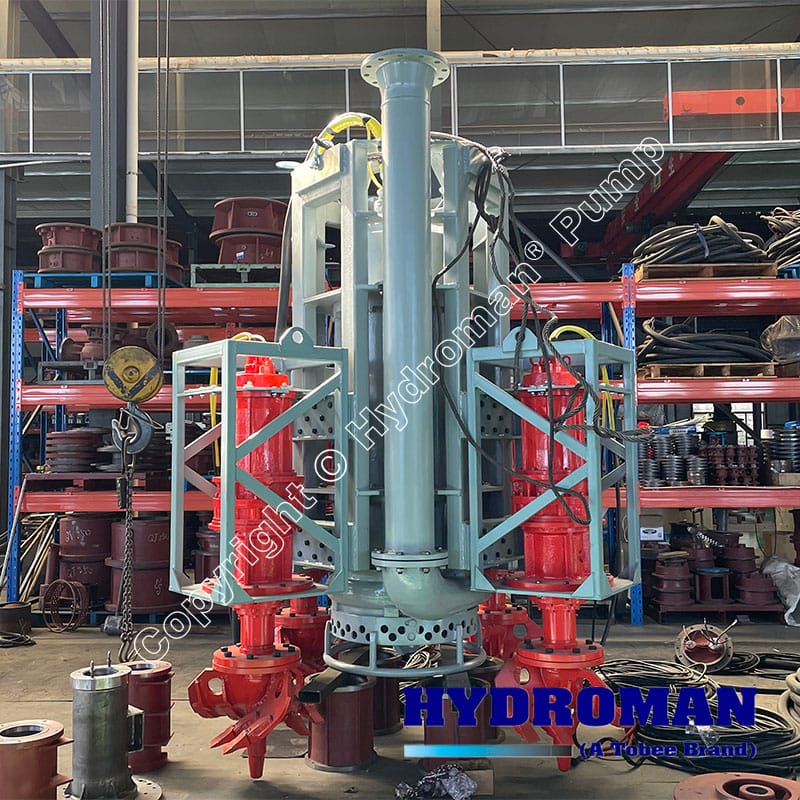
• Submerisble drainage pump can be provided as a partion of dredging pontoon barge solutions, wtih Hydroman® drainage soft pipe and Hydroman® vertical slurry pump, or installed on the equipment as excavator.
• Hydroman Sewage Disposal Pumps were dragging or pushing into the right place by the common using earthmoving equipments.
• Size: 50-400mm
• Capacity: 7-2400m3/h
• Head: 7-120m
• Power: 0.75-315kw
• Max. particle: 120mm
• Agitator or Cutter heads: Available
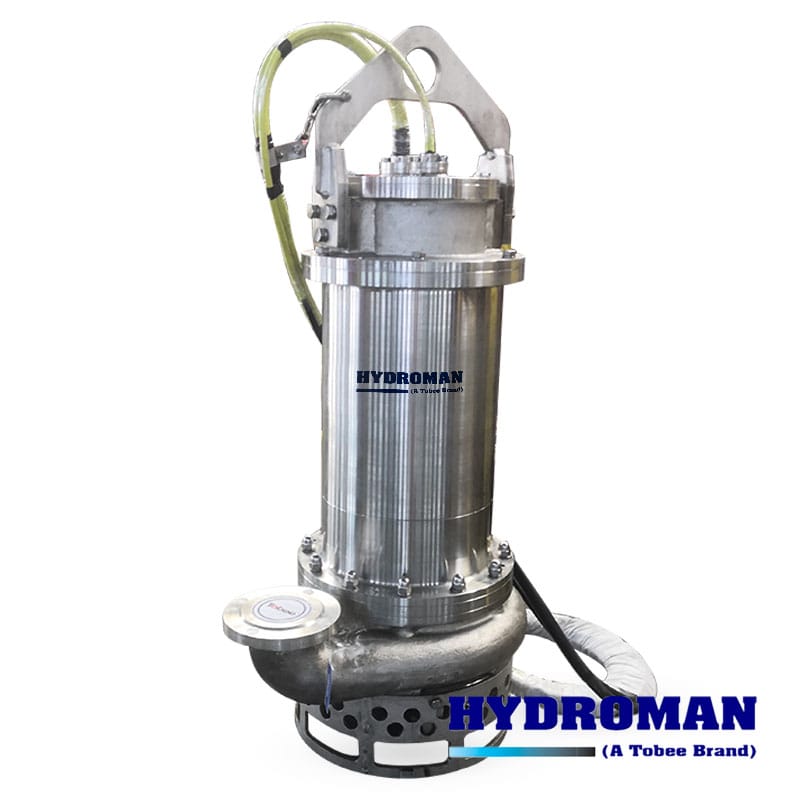
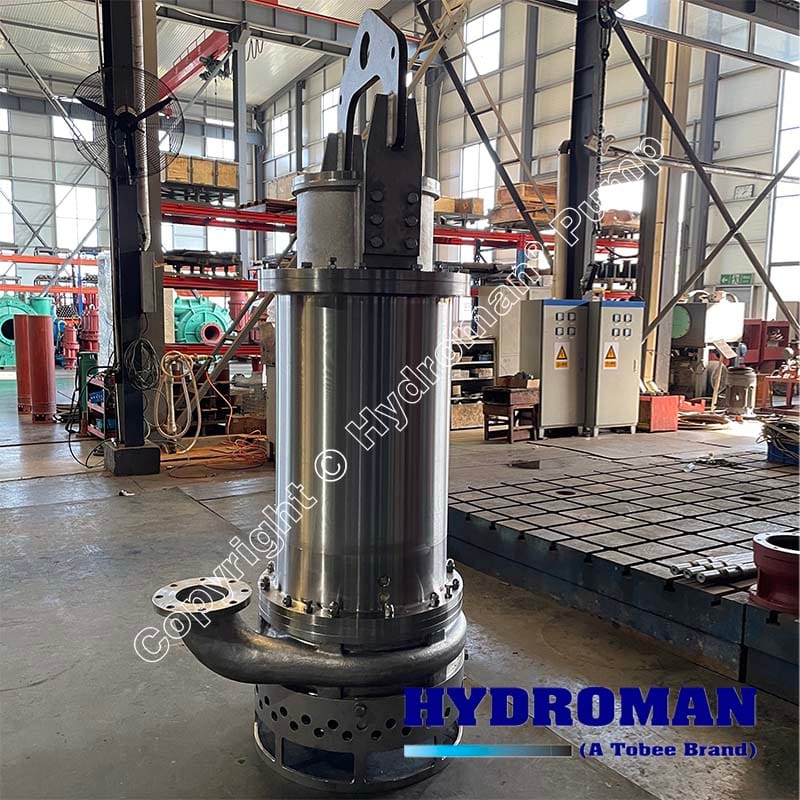
• Materials: High chrome, Hyperchrome, SS304, SS316L, Duplex SS etc
Hydroman Submerisble Mud Removal Pumps are the most wear pumps for under water to move fluid and sediments. These pumps can applied in many projects for removing mud or slurries:
1. Mining and quarrying
Application scenarios:
• Tailing treatment: pumping mud containing high concentration of metal particles and ore debris to the tailings pond.
• Mine drainage: quickly remove the groundwater and mud mixture that seeps in during the mining process.
• Ore washing operation: circulating mud when separating ore and impurities.
Technical advantages:
• Wear-resistant materials (such as high chromium alloy) cope with ore wear.
• High lift design meets the drainage needs of deep mines (up to 100 meters or more).
2. Construction and underground construction
Application scenarios:
• Foundation pit drainage: treat groundwater mixed with mud and sand during foundation excavation.
• Tunnel construction: pumping mud and rock debris in tunnel excavation (such as shield machine).
• Pile driving mud circulation: remove clay mud produced by pile foundation drilling.
Technical advantages:
• Anti-clogging design copes with impurities such as fibers and gravel.
• Compact structure adapts to narrow construction space.
3. Municipal and sewage treatment
Application scenarios:
• Sewage plant sludge treatment: extract concentrated sludge from sedimentation tanks to dewatering equipment.
• Pipeline desilting: clean up sediment and debris in sewers.
• Emergency drainage: quickly remove mud and water mixtures from streets and underground garages after heavy rain.
Technical advantages:
• Corrosion-resistant stainless steel (such as 316L) to deal with chemical corrosion of sewage.
• Equipped with a cutting system to crush fiber, plastic and other garbage (Grinder Pump model).
4. Agriculture and irrigation
Application scenarios:
• Fish pond desilting: remove organic sludge at the bottom of the breeding pond.
• Irrigation channel maintenance: pump out sediment deposited in the channel to ensure smooth water flow.
• Slurry transportation: treat high-concentration organic waste residues in biogas projects.
Technical advantages:
• Low-speed design reduces damage to activated sludge (suitable for organic matter transportation).
• Anti-entanglement impeller to deal with plant residues such as waterweed and roots.
5. Dredging and marine engineering
Application scenarios:
• Port desilting: remove sediment deposited at the bottom of the channel to ensure navigation depth.
• River management: suction of polluted sediment for environmental dredging.
• Submarine pipeline laying: remove seawater-sediment mixture when excavating trenches.
Technical advantages:
• Seawater corrosion-resistant design (such as duplex stainless steel or coating protection).
• Large flow configuration (up to 2000 m³/h) to meet large-scale dredging needs.
6. Oil and gas industry
Application scenarios:
• Drilling mud circulation: conveying a mixture of cuttings and clay in drilling fluid.
• Oil tank cleaning: suction of oily sludge at the bottom of the oil tank.
• Oilfield wastewater treatment: transfer of oily and sandy production wastewater.
Technical advantages:
• Explosion-proof certification (ATEX/IECEx) for flammable and explosive environments.
• High temperature resistant sealing system (adaptable to media above 60°C).
7. Industrial wastewater treatment
Application scenarios:
• Chemical plant sludge treatment: transporting sludge containing acid, alkali or toxic components.
• Steel plant sludge pool cleaning: extracting iron oxide scale and impurities from steel mill wastewater.
• Paper mill waste slag treatment: treating high-fiber sludge left over from pulp.
Technical advantages:
• Customized material selection (such as Hastelloy and titanium) to cope with highly corrosive media.
• Variable frequency control enables precise flow regulation.
 +86 189 3110 6396 (24/7 Support)
 Inquiry@tobeepump.com (Send your mud analysis for material recommendations)
Hydroman® is a professional submersible pumps supplier, mainly designed Slurry Mud Pump, Submerisble Sludge Pump, Electric Drainage Pumps, Vertical Sand Pump, Hydroman Sewage Disposal Pumps, Industrial Mud Removal Pumps for your mining, offshore, cannals applications.
Submitted successfully
Your submission has been received. Thanks for your time
 FR(EUR)
 CN(CNY)
 GB(GBP)
 AU(AUD)



Reviews
0%
0%
0%
0%
0%
Share your thoughts with other customers
Write a Review