


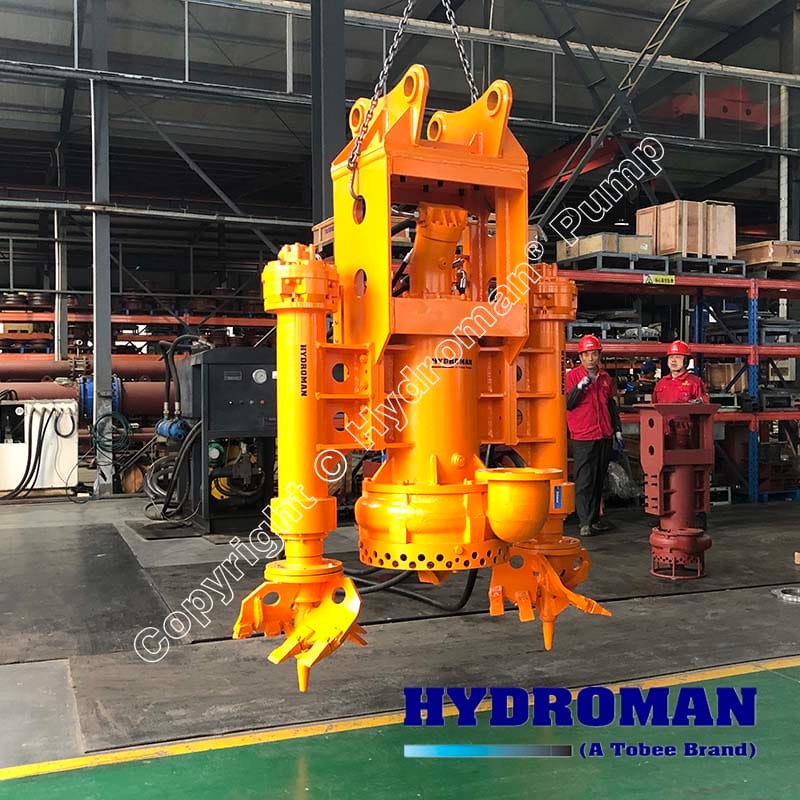
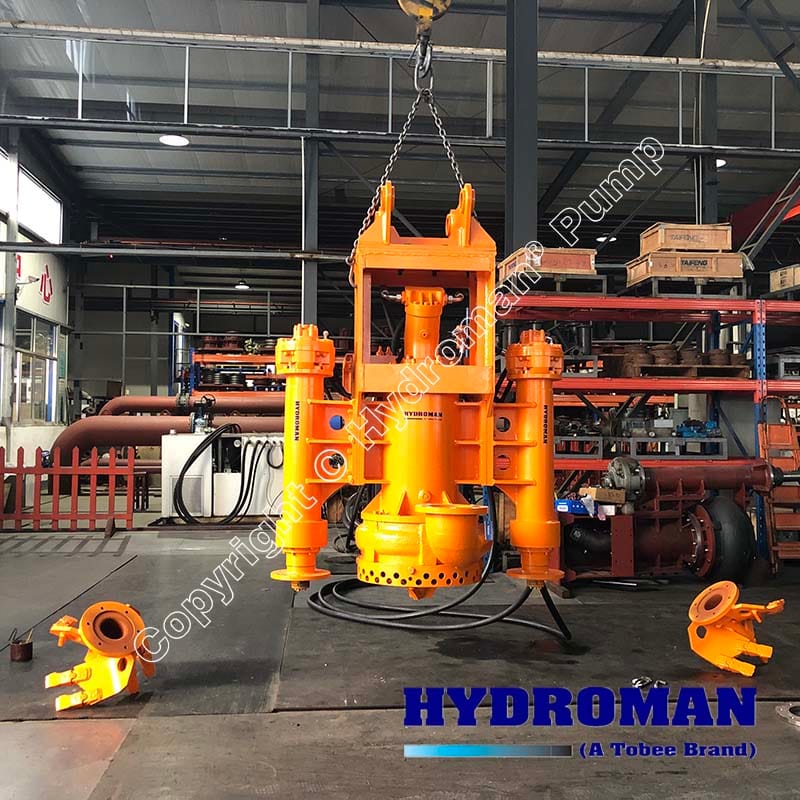

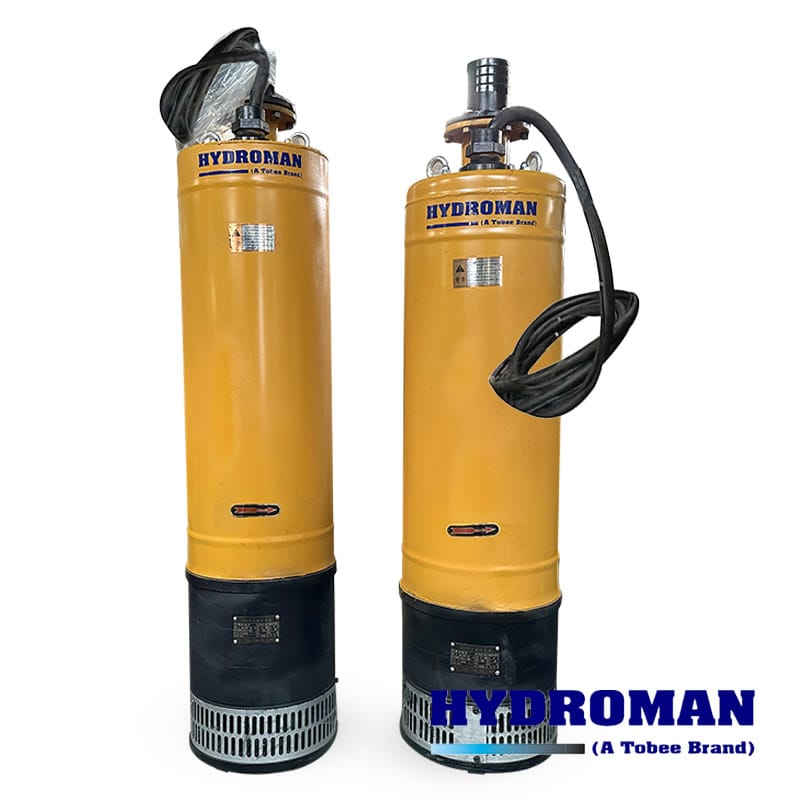
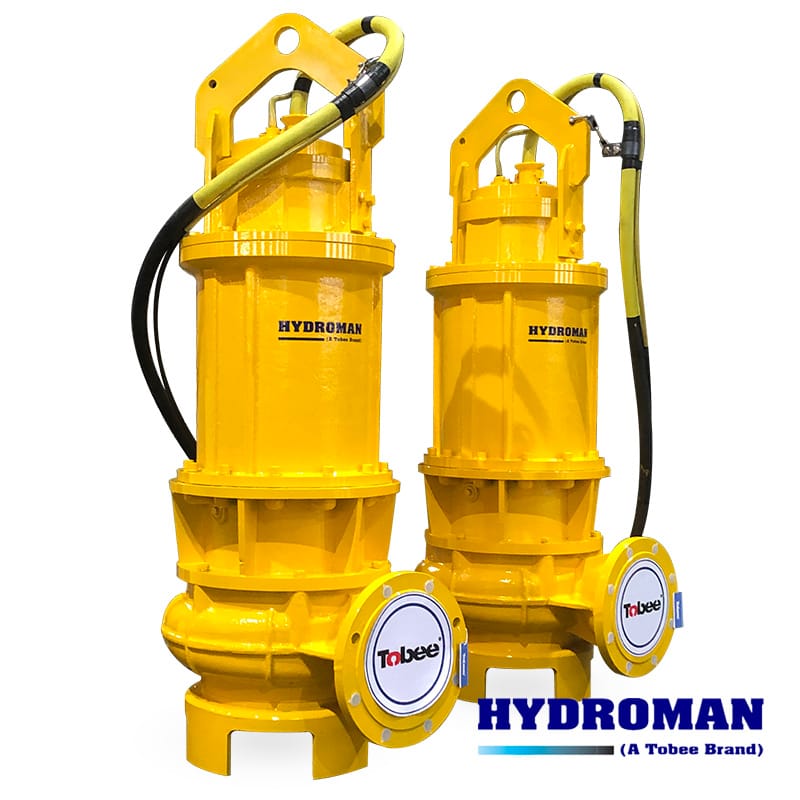
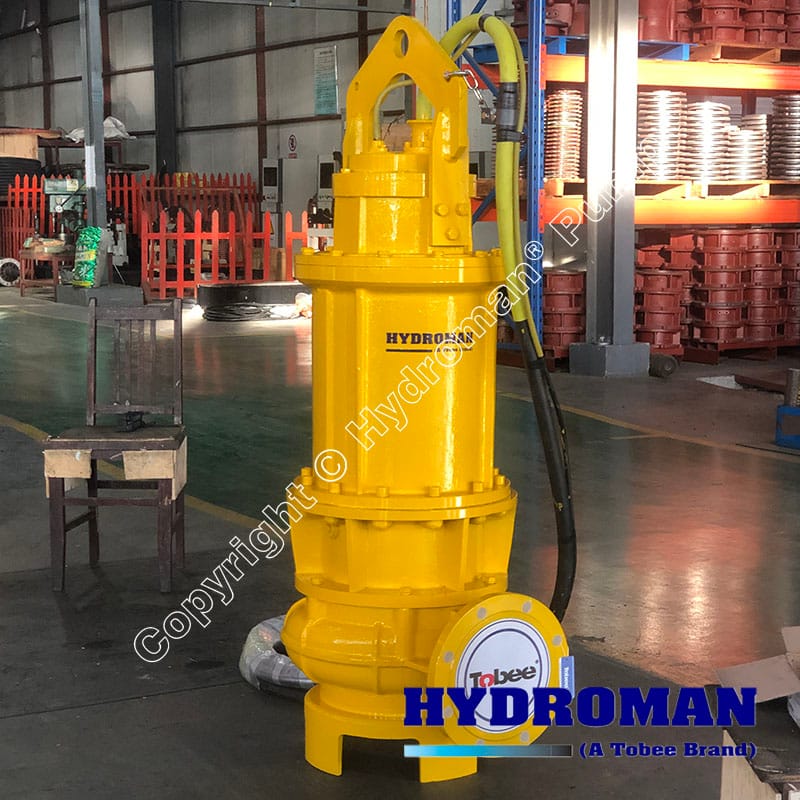
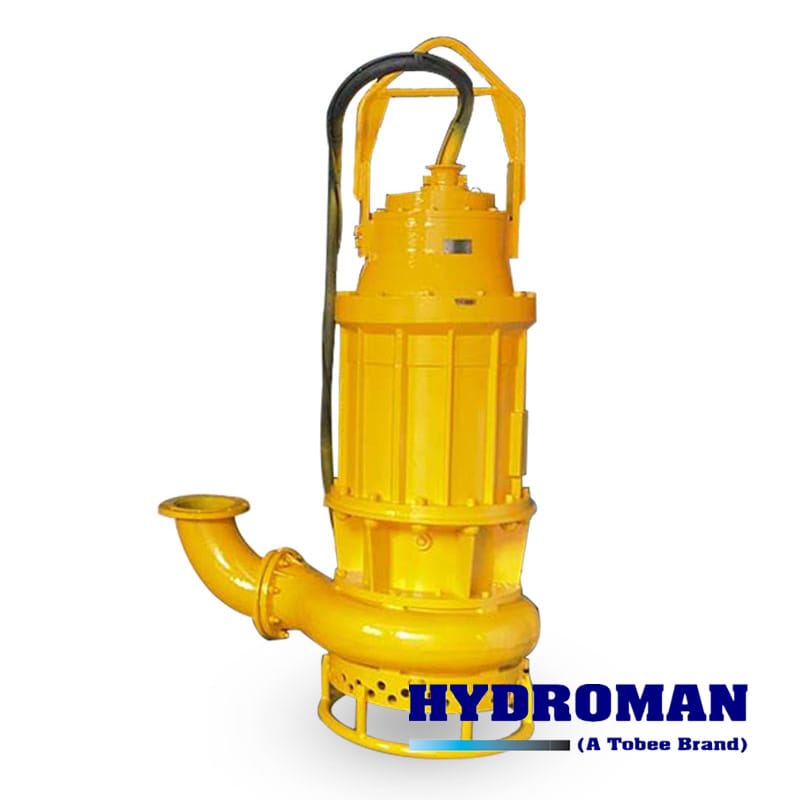
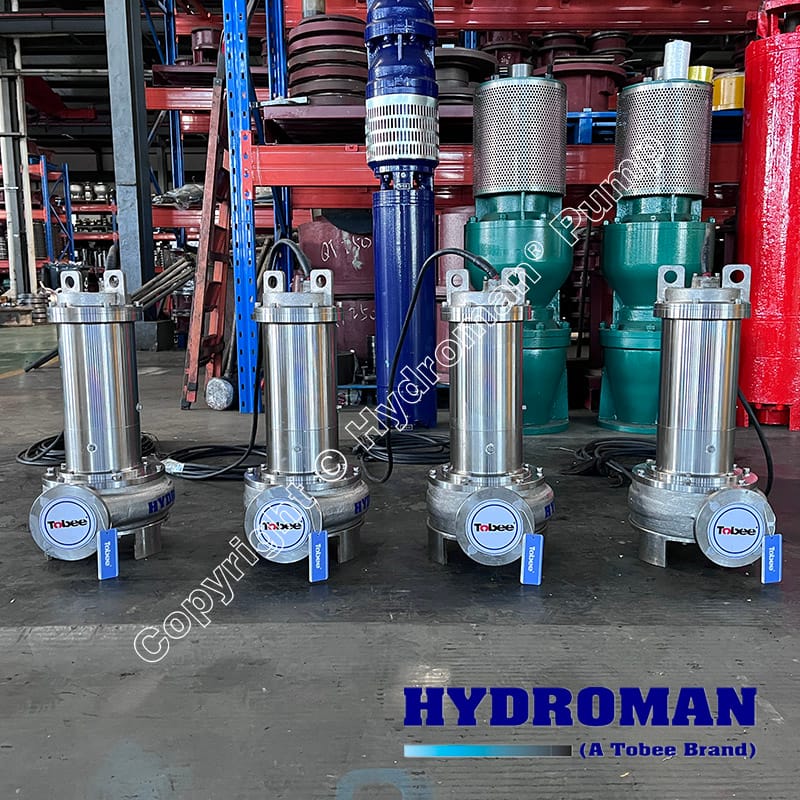
Tackling the abrasive, dense slurries inherent in rare earth mining demands specialized equipment. The Hydroman® Heavy Duty Submersible Slurry Pump for Hydraulic Excavator is engineered precisely for this challenge. This robust system is the ultimate Submersible Slurry Pump for Rare Earth Mining Applications, designed to be mounted directly onto your excavator. It excels as a Hydraulic Excavator Slurry Pump for Mineral Slurry Extraction, efficiently clearing sand, sediment, viscous slurry, wastewater, and processing waste. Its Robust Slurry Pump System for Rare Earth Sediment Handling ensures maximum uptime and mineral recovery in the planet's most demanding environments. This Industrial Submersible Pump for Rare Earth Ore Slurry Transfer is indispensable for modern, efficient rare earth operations worldwide.
FAQ:
Q: Why use a submersible pump on an excavator for rare earths?
A: It combines the excavator's mobility and reach with direct pumping power, allowing operators to pump thick, abrasive slurries right from the source (settling ponds, tailings dams, dredge sites) without relocation delays, significantly boosting efficiency.
Q: What makes Hydroman® pumps suitable for abrasive rare earth tailings?
A: They feature ultra-wear-resistant materials (like high-chrome alloys) in critical components, a patented vortex design minimizing contact with abrasives, and a rugged construction built for the high solids content and punishing conditions of rare earth waste streams.
Q: Can this pump handle high-density rare earth ore slurries?
A: Absolutely. The Hydroman® pump's high-torque, low-RPM design and large agitator are specifically engineered to lift and move exceptionally dense, viscous mixtures common in rare earth beneficiation and tailings management, where standard pumps fail.
Conquering Global Rare Earth Mining Challenges
Rare earth elements (REEs) are vital for advanced technologies, but their extraction presents unique hurdles. Mining generates vast quantities of abrasive mineral slurries, heavy tailings laden with residual chemicals, and process wastewater. Traditional pumping solutions often succumb to rapid wear, clogging, and inefficiency, leading to costly downtime and lost recovery potential.
Mounted directly onto your hydraulic excavator, this Excavator Mounted Slurry Pump for Harsh Mining Environments transforms your machine into a supremely versatile pumping powerhouse. Operators can precisely position the pump intake directly into the thickest sediment, slurry pit, or tailings pond, pumping material over significant distances or heights to processing plants, dewatering stations, or tailings storage facilities (TSFs). This eliminates the need for multiple pieces of equipment or complex priming systems, drastically improving operational fluidity.
Applications Driving Rare Earths Productivity
• Efficient Ore & Tailings Transport: As a High Performance Slurry Pump for Rare Earth Tailings Recovery, it excels in moving raw ore slurry from mining faces and, crucially, transporting the abrasive residue (tailings) to storage facilities. Its ability to handle high solids content minimizes water usage and ensures safe, efficient tailings disposal, a critical environmental consideration.
• Settling Pond & Tailings Dam Management: Essential for dredging accumulated sand and sediment from settling ponds and reclaiming water. It efficiently manages TSFs by pumping tailings slurry for deposition or recycling water from decant ponds, supporting sustainable water management.
• Beneficiation & Processing Support: Transfer ground ore slurry between processing stages (e.g., to flotation cells or leaching tanks) and handle the dense concentrates produced during filtration and thickening.
• Site Cleanup & Water Reclamation: Vital for environmental compliance, cleaning sumps, trenches, and process areas contaminated with slurry or wastewater. Effectively reclaims process water from various ponds for reuse.
• Emergency Spill Response: Provides rapid deployment capability for containing and recovering chemical spills or slurry overflows, minimizing environmental impact.
• Unmatched Wear Resistance: Engineered with premium abrasion-resistant materials to withstand constant exposure to highly abrasive rare earth particles, extending service life and reducing maintenance frequency/costs.
• Clog-Free Operation: The patented open vortex design and powerful agitator easily pass large solids and handle stringy materials that would jam conventional pumps, ensuring continuous operation.
• High Solids Handling: Capable of pumping slurries with exceptionally high solids content and density, crucial for thick tailings and concentrated ore streams.
• True Heavy-Duty Construction: Robust components and a design focused on reliability deliver consistent performance under extreme loads in mines across Australia, Africa, North America, and Asia.
• Maximized Mineral Recovery: Efficiently moves valuable ore slurries and facilitates thorough tailings reprocessing, ensuring optimal yield from your resource.
Don't let abrasive slurries, stubborn tailings, or inefficient pumping slow down your critical rare earth mining or processing project. The Hydroman® Heavy Duty Submersible Slurry Pump for Hydraulic Excavator delivers the rugged reliability, exceptional performance, and operational flexibility you demand. Experience reduced downtime, lower operating costs, enhanced recovery rates, and superior environmental management.
Contact Hydroman® NOW to discuss your specific requirements and discover how our specialized pumping solution can revolutionize your rare earth sediment, slurry, and wastewater handling. Boost your productivity and profitability – Get Your Quote Today!
 Sara Liang
 +86 189 3110 6396 (Whatsapp/Wechat)
 Inquiry@tobeepump.com
Submitted successfully
Your submission has been received. Thanks for your time
 FR(EUR)
 CN(CNY)
 GB(GBP)
 AU(AUD)




Reviews
0%
0%
0%
0%
0%
Share your thoughts with other customers
Write a Review