
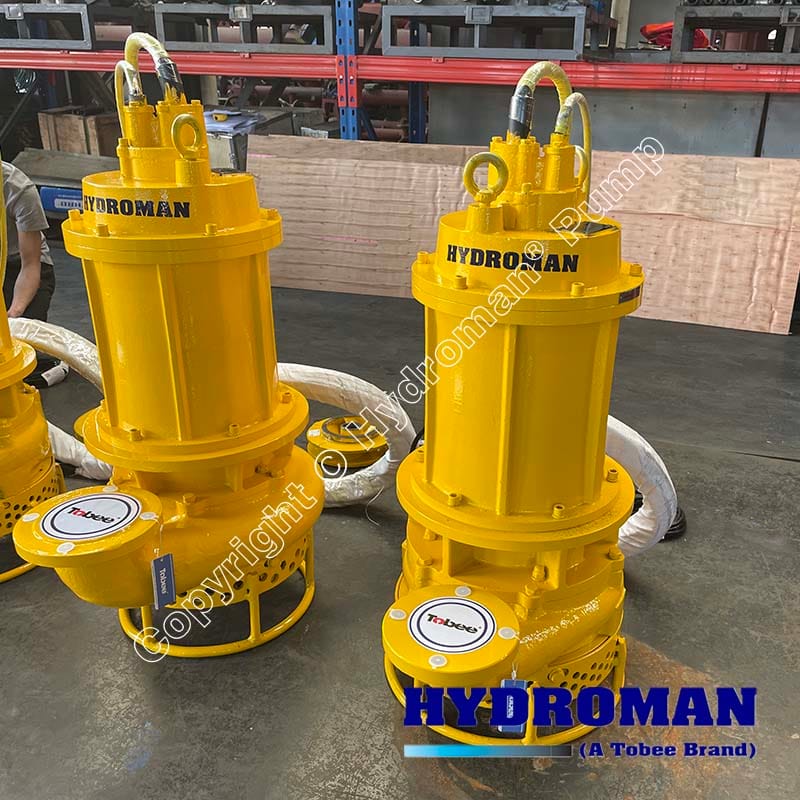
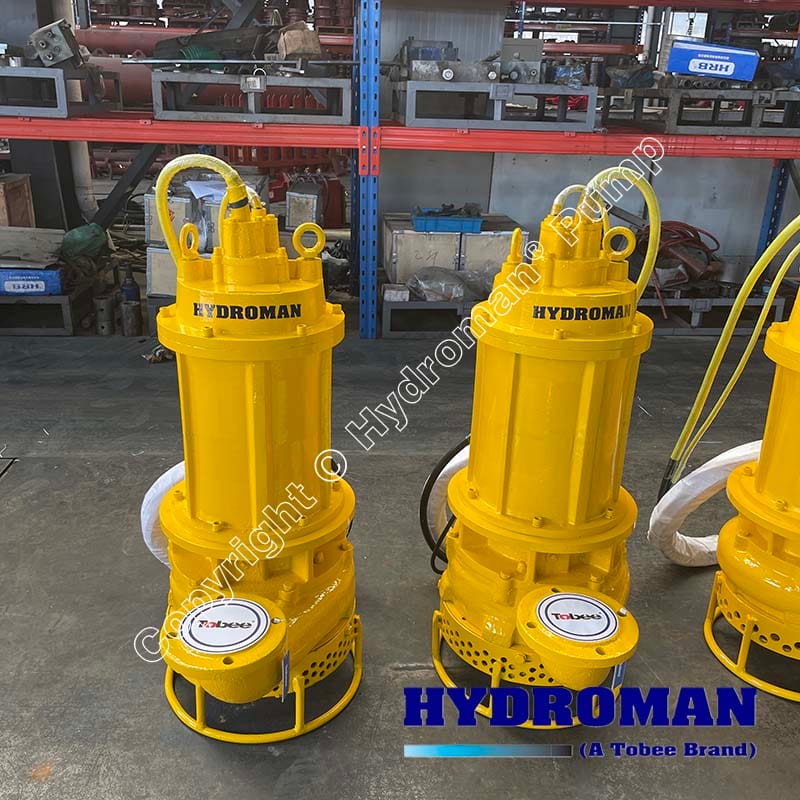
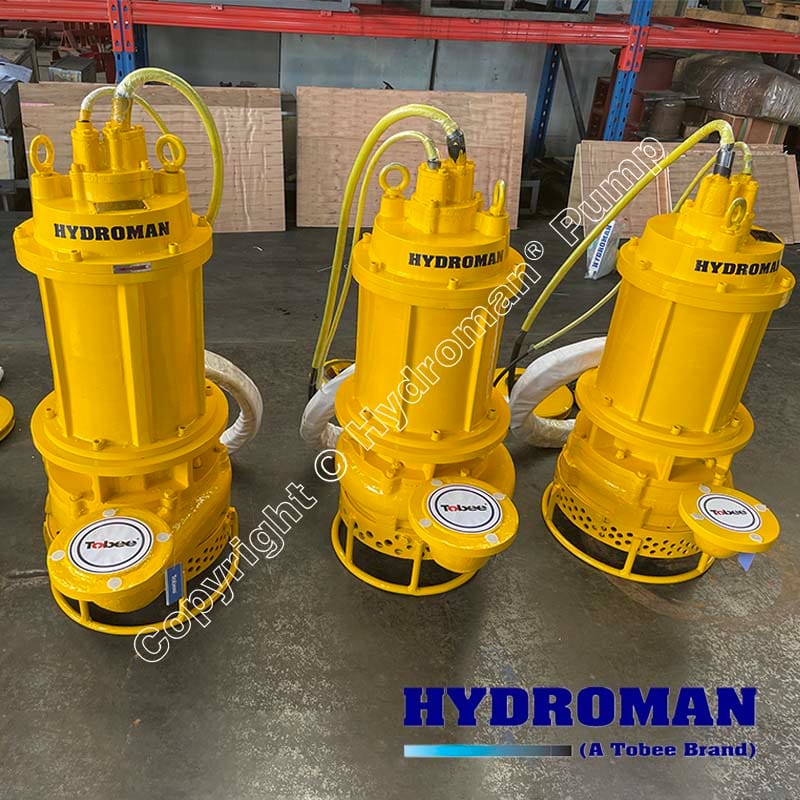
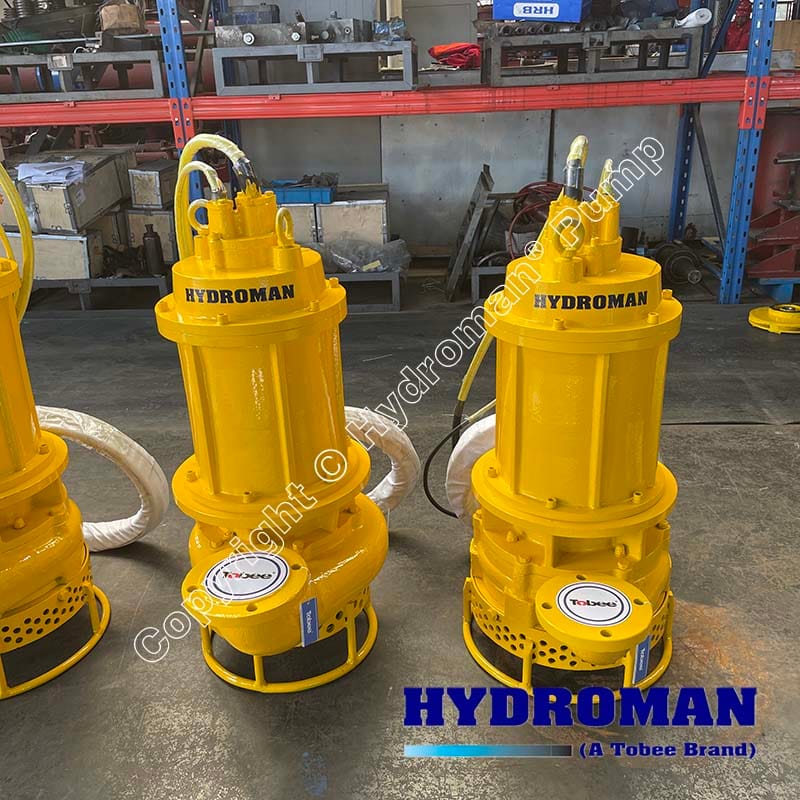
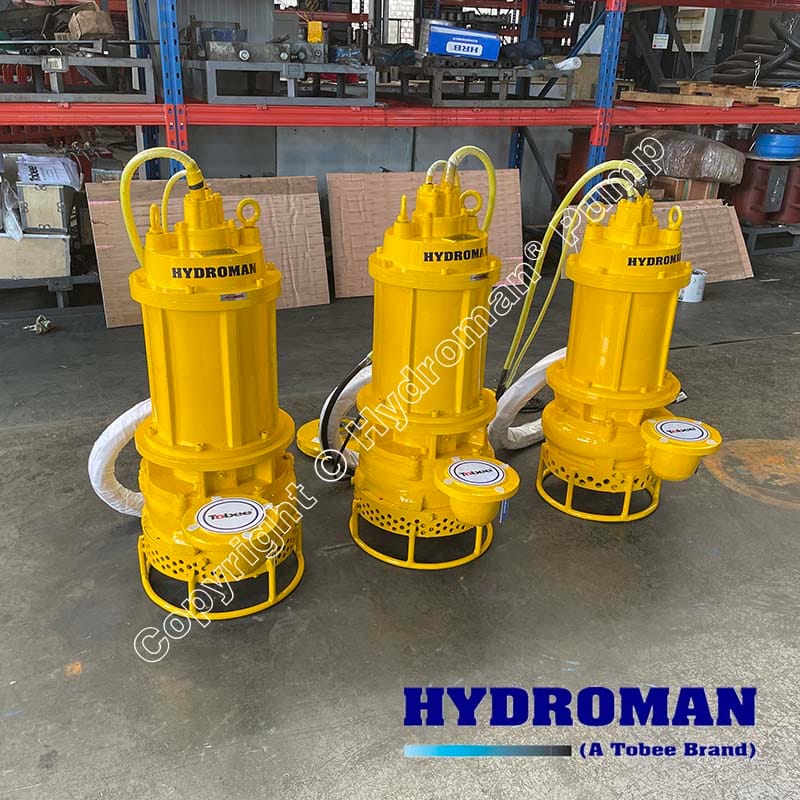
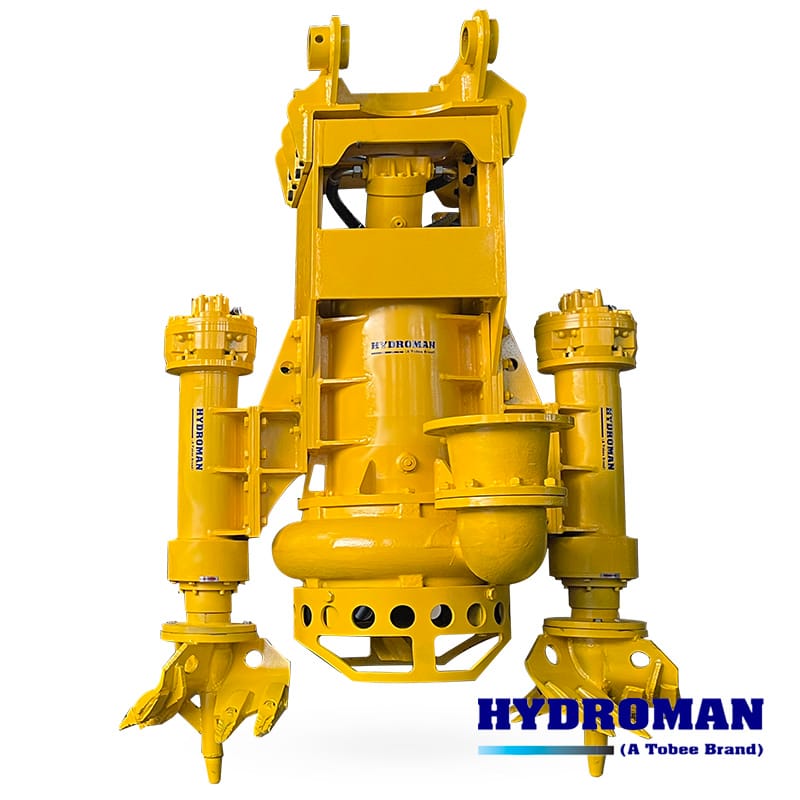
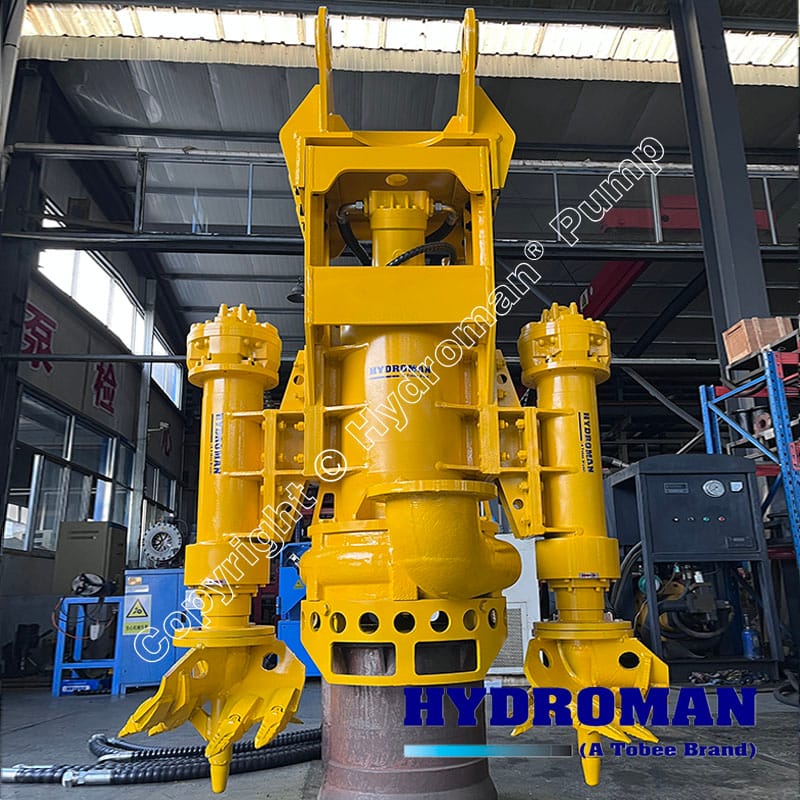
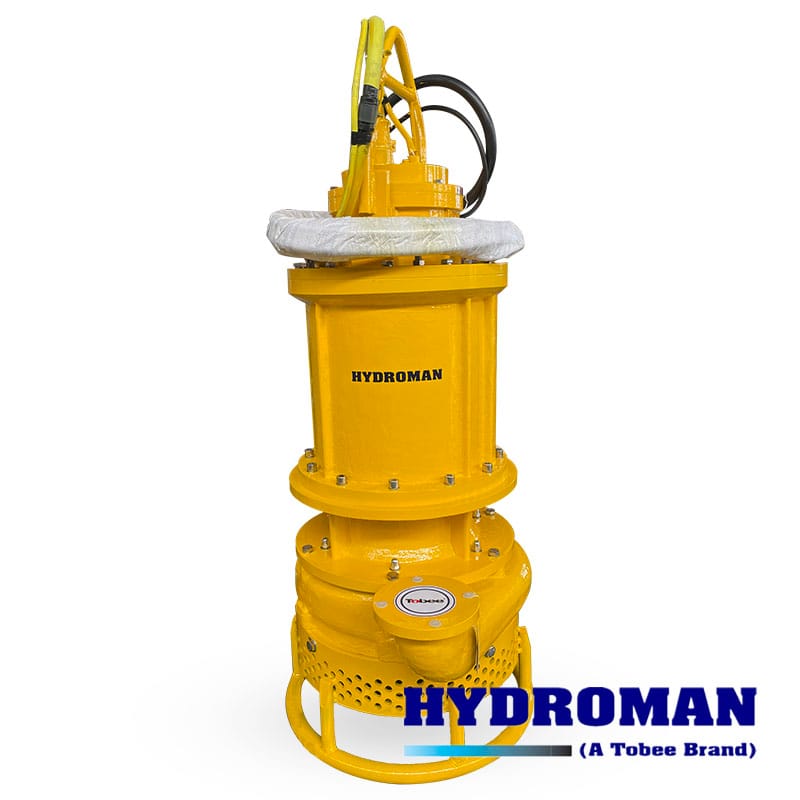
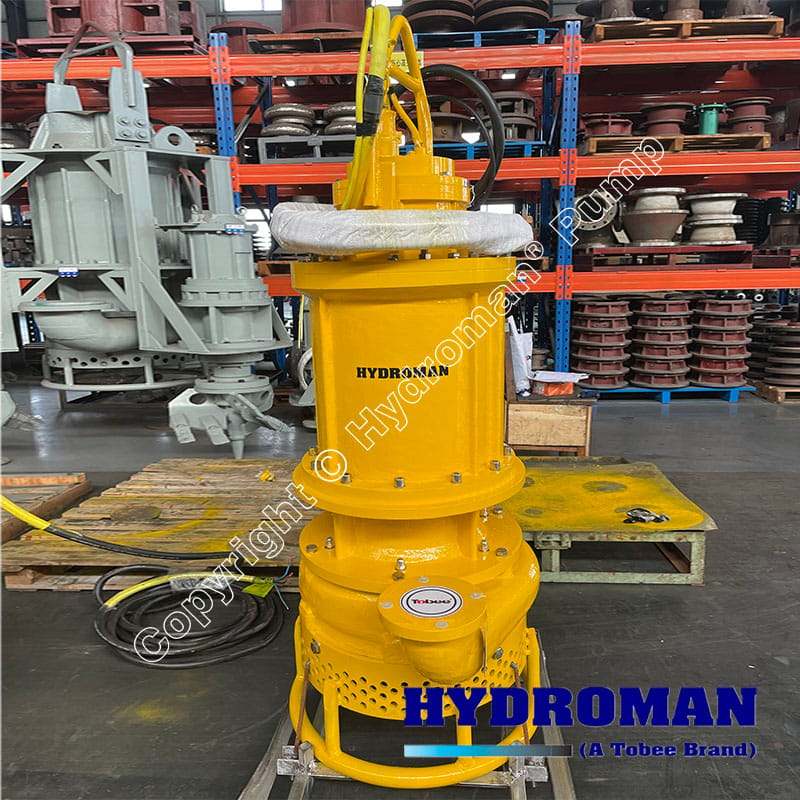
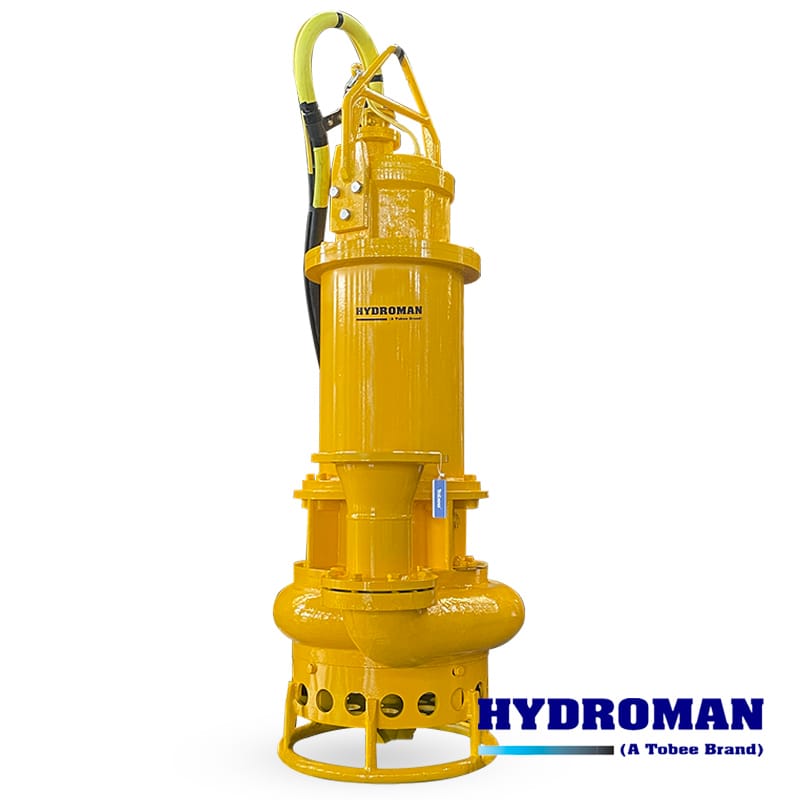
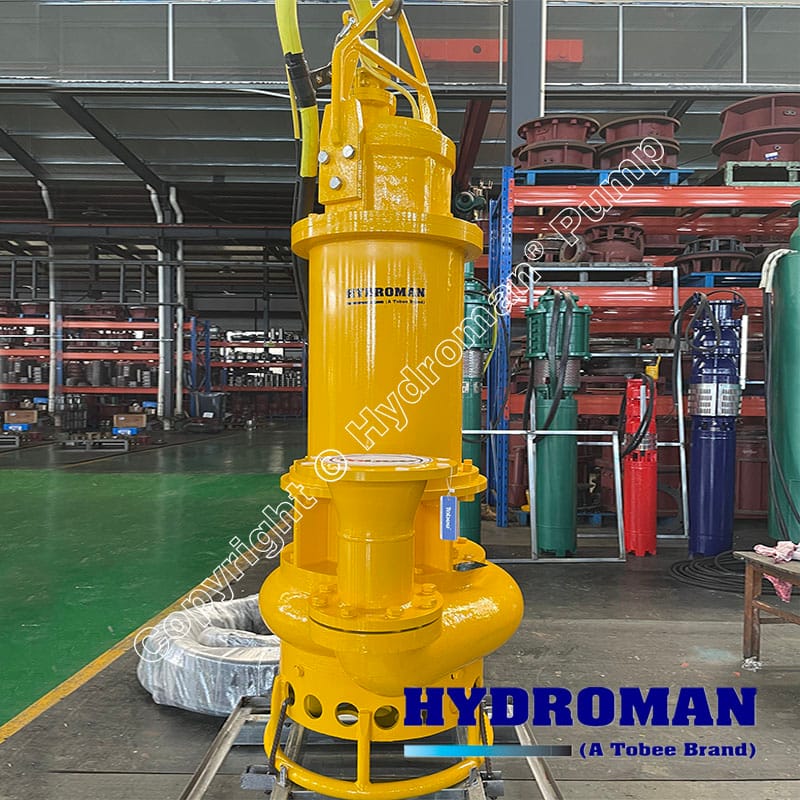
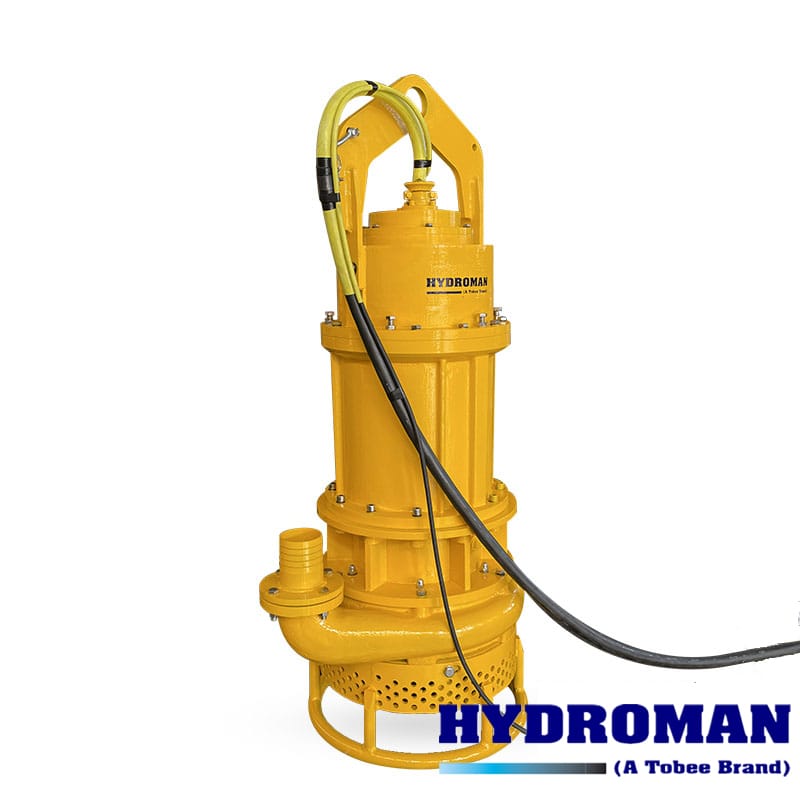
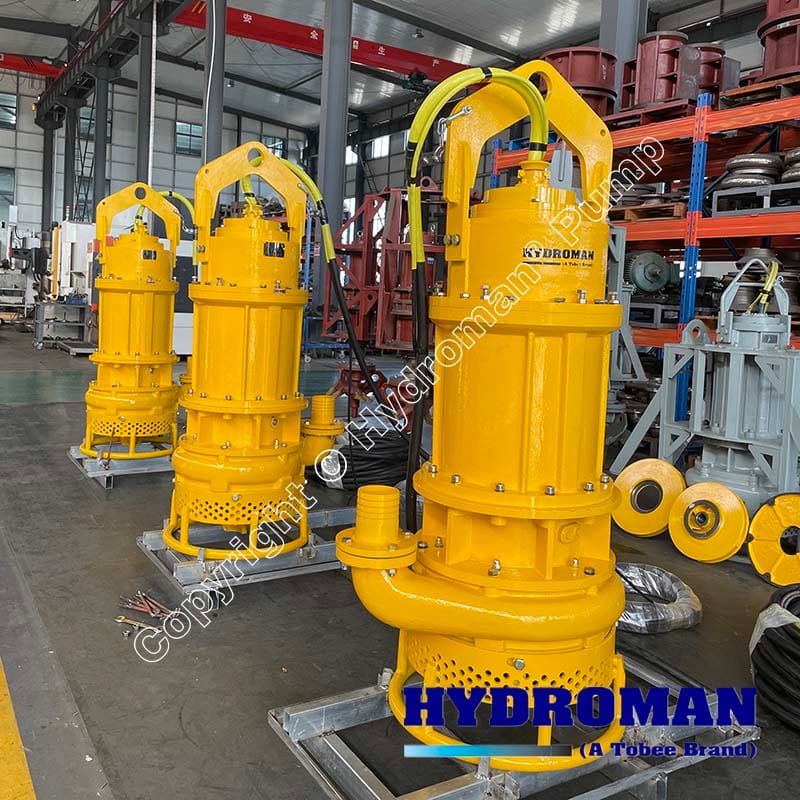
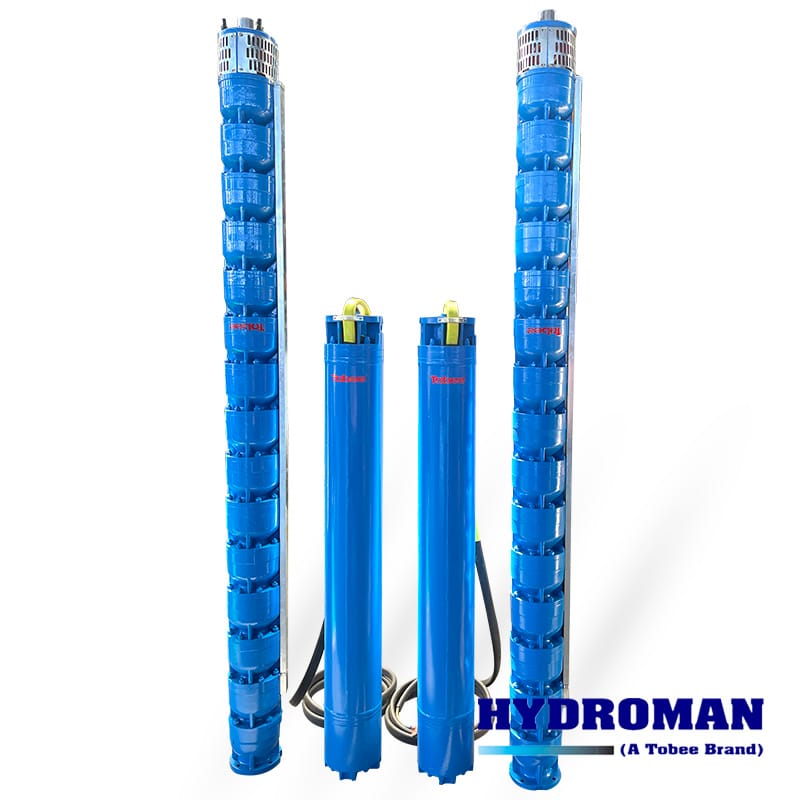
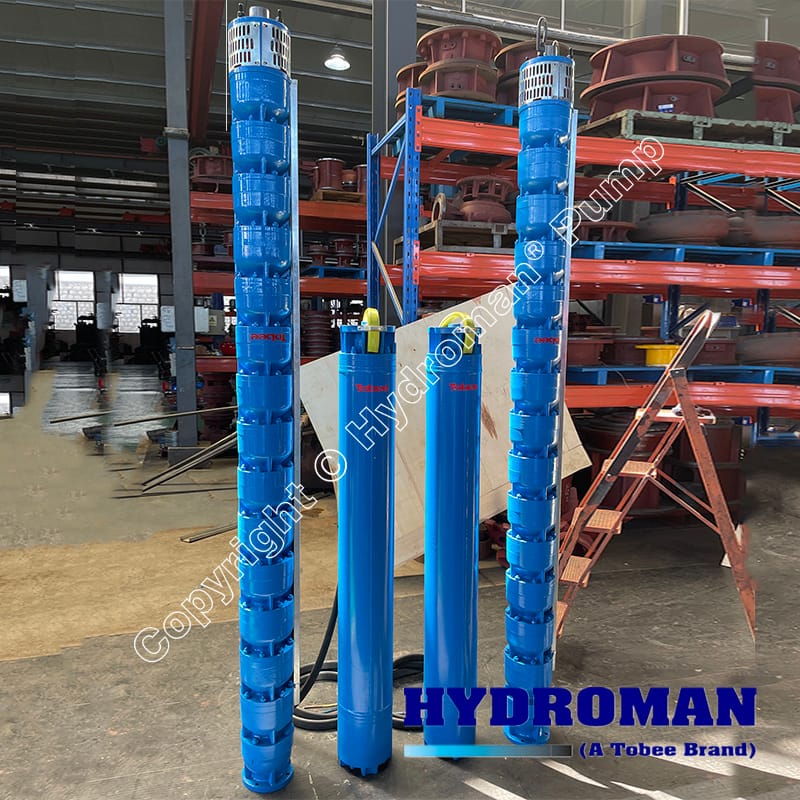
Tired of downtime and inefficiency in your rubidium mining slurry handling? Meet the Hydroman® Strong Delivery Capacity Submersible Slurry Sand Pump with Agitator – the Electric Driven Submersible Slurry Pump for Rubidium Mining engineered for relentless performance. This High Capacity Submersible Sand Pump with Agitator System is built to conquer the toughest underwater challenges, pumping dense mixtures of slurry, gravel, sand, mud, and critical rubidium ore with unmatched power. As a cornerstone Durable Electric Submersible Slurry Pump for Mining Industry, it excels as the ultimate Submersible Slurry Sand Pump for Handling Rubidium Ore, delivering the Strong Delivery Power essential for continuous operation. Choose the Reliable Electric Submersible Slurry Pump for Sand Extraction and transform your material handling.
The Hydroman® Strong Delivery Capacity Submersible Slurry Sand Pump with Agitator operates fully submerged, a critical design for deep sumps, pits, and settling ponds common in rubidium extraction. Its Strong Delivery Power isn't just a claim; it's a result of robust hydraulic engineering enabling the pump to efficiently move slurries with extremely high solids content – often exceeding 60-70% by volume. This means handling everything from fine rubidium-bearing sediments and sandstones to coarse gravel and challenging big solids with exceptional flow rates.
What truly sets this pump apart is its integrated Agitator System. Unlike standard submersible pumps that can struggle with settled solids, the Hydroman® features a powerful bottom-mounted agitation impeller. This key component actively churns the pump intake area, spraying deposited sludge and compacted sediments into turbulent flow. This crucial action:
• Prevents Clogging: By constantly re-suspending solids before they can settle and block the suction.
• Boosts Concentration: Ensures a consistent, high-density slurry enters the pump, maximizing the volume of valuable rubidium ore transported per hour.
• Increases Suction Efficiency: Significantly improves the pump's ability to draw in material, especially critical when clearing thick mud or deeply settled waste. This translates directly to smoother operation and less manual intervention.
• Simplifies Operation: Effectively automates the process of keeping solids in suspension, streamlining pumping tasks like sump dewatering or tailings pond management.
Rubidium mining processes, whether involving acid leaching, roasting, or other hydrometallurgical techniques, generate highly abrasive and often corrosive mixtures. The Hydroman® pump is purpose-built for these demanding applications:
• Primary Ore Slurry Transport: Efficiently moving the initial rubidium-containing ore slurry from excavation or collection points to primary processing plants.
• Process Slurry Circulation: Handling intermediate slurries during leaching or washing stages within the processing circuit.
• Tailings Management: Reliably pumping waste slurries (tailings) to disposal ponds or for further treatment. Its ability to handle settled solids is invaluable here.
• Sump & Pit Dewatering: Rapidly clearing water mixed with sand, mud, and fine solids from mining excavations and collection points.
• Sediment & Sludge Removal: Excelling in cleaning out accumulated sediments, sandstones, and sludge from settling tanks, channels, and containment areas.
Reliability is non-negotiable in mining. The Durable Electric Submersible Slurry Pump for Mining Industry lives up to its name through superior construction:
• Wear-Resistant Alloys: Critical wet-end components like the agitator impeller, main pump impeller, and volute casing are typically cast from high-chrome alloys or specialized abrasion-resistant materials to withstand relentless sand, gravel, and ore particle impact.
• Heavy-Duty Electric Drive: The Electric Driven motor is sealed and protected for submerged operation, offering reliable power transmission and often easier integration than hydraulic systems. Designed for Vertical Use, it delivers power efficiently to both the pump and the agitator below.
• Robust Sealing: Advanced double mechanical seals, often with oil-lubricated chambers, provide exceptional protection against water and abrasive slurry ingress, extending bearing and motor life dramatically.
• Reinforced Bearings: Oversized, heavy-duty bearings handle the significant radial and axial loads generated by pumping dense slurries and the agitator's action.
Choosing the Hydroman® Strong Delivery Capacity pump means investing in:
• Maximum Production Uptime: Reduced clogs and robust construction minimize costly stoppages.
• Lower Total Cost of Ownership: Exceptional wear life and reduced maintenance needs translate to significant savings over time.
• Operational Simplicity: The integrated electric drive and agitator create a powerful, self-contained solution.
• Proven Performance: Hydroman® engineering is trusted in the most demanding mining and industrial applications globally.
Q: Why is an electric-driven pump preferred over hydraulic for this application?
A: Electric-driven pumps like the Hydroman® offer several advantages: generally higher efficiency, simpler installation without hydraulic power units/hoses, reduced fire risk (no hydraulic oil), easier speed control (with VFDs), and often lower operational noise. They provide reliable, consistent power directly to the pump and agitator.
Q: What size solids can the Hydroman® pump with agitator handle?
A: While specific models vary, Hydroman® Strong Delivery Capacity Submersible Slurry Sand Pumps with Agitator are typically designed to handle particles up to 50-70mm in diameter, depending on the model and volute design. The agitator is crucial for breaking up smaller agglomerations and preventing larger solids from bridging and blocking the inlet.
Q: How does Hydroman® ensure the pump withstands the extreme abrasion in rubidium mining?
A: Hydroman® prioritizes wear resistance. Key components utilize high-chrome white iron (HCWI) alloys, specialized manganese steels, or even elastomer linings where appropriate. The exact material is chosen based on the specific slurry abrasiveness and corrosion potential. Combined with robust hydraulic design minimizing internal turbulence and velocity, this ensures exceptional service life.
Don't let challenging slurries slow down your rubidium extraction. The Hydroman® Strong Delivery Capacity Submersible Slurry Sand Pump with Agitator delivers the High Capacity, Strong Delivery Power, and Reliable Electric operation you demand. Its Durable construction and unique bottom Agitator System make it the definitive solution for efficiently handling rubidium ore, gravel, sand, mud, waste, and sediments. Maximize your productivity and minimize downtime.
Upgrade your slurry handling today! Contact Hydroman® to discuss your specific rubidium mining requirements and request a quote for the ultimate in submersible pumping performance.
 Sara Liang
 +86 189 3110 6396 (Whatsapp/Wechat)
 Inquiry@tobeepump.com
Submitted successfully
Your submission has been received. Thanks for your time
 FR(EUR)
 CN(CNY)
 GB(GBP)
 AU(AUD)


Reviews
0%
0%
0%
0%
0%
Share your thoughts with other customers
Write a Review